Qué buscas?
A custom Inconel heat shield blank is not simply a smaller piece cut from a larger Alloy 625 sheet. The blank is the starting geometry from which the finished shield will be formed. If its outline, pattern direction, holes or trimming allowance are wrong, later forming operations cannot reliably correct the problem.
This is particularly important with nickel-alloy heat shield material. The material cost makes unnecessary scrap expensive, while a blank that is too tightly dimensioned can create more serious costs through failed forming trials, misaligned mounting features and rejected finished parts.
BSTFLEX supplies Alloy 625 Inconel heat shield material as barrier sheet, custom-cut patterns and formed heat shield components. Available processing options include laser or waterjet cutting, stamping and forming, holes, slots, tabs and optional edge finishing according to project requirements.
An Inconel heat shield blank is a flat or partially prepared piece of Alloy 625 material intended for subsequent forming, assembly or installation.
Depending on the project, the blank can be:
The word “blank” should not be confused with a finished formed shield.
A blank defines the starting material geometry. The finished part defines the geometry after bending, drawing, folding, trimming or other forming operations.
For a repeat OEM program, it is useful to distinguish three manufacturing stages:
| Stage | What It Defines | Typical Purchasing Information |
|---|---|---|
| Raw Alloy 625 sheet | The incoming flat metal material | Alloy, condition, base-metal thickness, sheet dimensions and surface |
| Heat shield blank | The profile cut before forming | Flat outline, datums, orientation, holes, slots and process allowance |
| Finished heat shield | The installed three-dimensional component | Formed surfaces, flanges, tabs, mounting points, edges and final tolerances |
Using one drawing for all three stages can create ambiguity. A dimension may be interpreted as a raw sheet size by one supplier and a finished component dimension by another.
For complex components, provide both the flat blank drawing and the finished-part drawing.
Blank development should begin with the finished component, not with the size of material already available.
Review every feature that consumes material during forming:
A finished shield measuring 300 mm across does not necessarily require a 300 mm-wide blank. Material may be needed to form side returns, mounting features or edge treatments.
Conversely, adding a large arbitrary allowance around every edge is also inefficient. The additional material should correspond to a real manufacturing requirement.
Fabrication allowance is additional material intentionally included in the blank because the downstream manufacturing process requires it.
Several different allowances may be involved.
A bend changes the relationship between the flat blank and the finished component. The developed length must account for the actual bend geometry rather than simply adding the finished flange dimensions together.
The required development depends on the selected material, thickness, bend radius and forming process. Do not apply one generic bend allowance to every Alloy 625 heat shield.
Deep or complex shapes may require additional material to flow during forming. The blank outline may therefore extend beyond the final component perimeter in selected areas.
Some components are more repeatable when they are formed first and trimmed to the final edge afterward.
Where this method is used, show both:
This prevents the temporary process material from being mistaken for part of the final shield.
A manufacturing process may require temporary areas for locating, holding or transferring the blank.
If these areas will later be removed, identify them clearly on the process drawing rather than leaving them as undocumented scrap.
For embossed Inconel heat shield material, the word “thickness” can create confusion.
At least three measurements can be relevant:
The base-metal thickness describes the Alloy 625 material itself.
The embossed height describes the three-dimensional surface profile formed into that metal.
The finished shield envelope includes subsequent bends, curves and other component geometry.
These measurements should be listed separately where they are controlled.
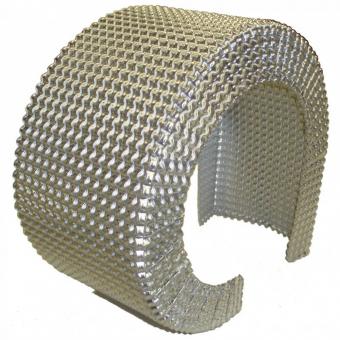
If the heat shield uses an embossed or dimpled surface, the pattern is part of the blank specification.
Do not identify the material only as:
“Embossed Inconel 625.”
A production requirement can also need:
This becomes particularly important when mounting features, seams or tight bends should not pass through an uncontrolled embossed area.
For additional background on embossed metal construction, see why embossed metal is used for automotive heat shields.
When a repeating embossing pattern has a controlled direction, rotating blanks purely to maximize material utilization may not be acceptable.
The drawing should identify orientation relative to a defined datum.
Useful references include:
If orientation does not matter, state that as well. Removing unnecessary restrictions can improve material utilization.
Some component features can be easier to control when they are located in a defined flat area rather than directly over an embossed profile.
Examples can include:
Whether a flat zone is needed depends on the tooling and finished design. It should not be added automatically.
If the feature is critical, show the permitted relationship between the embossing and the feature on the drawing.
There is no universal answer.
Pre-cut holes can simplify later processing, but forming may move or distort them relative to the finished component datums.
Post-forming holes can be located from the final geometry, but the finished part must be supported and referenced accurately during the operation.
For each mounting feature, determine:
A hole that is correct in the flat pattern but incorrect after forming is not a successful blank.
Slots can be useful where the component design needs installation adjustment or controlled movement. They should not be added simply to compensate for inaccurate blank geometry.
Specify:
If a slot is intended to accommodate thermal expansion, the complete mounting arrangement should be reviewed as an assembly.
A mounting tab is part of the heat shield structure, not an accessory added after the main panel has been designed.
The blank drawing should show:
Narrow tabs can be sensitive to cutting damage and local forming strain. Inspect the actual formed feature during prototype approval instead of approving only its flat dimensions.
BSTFLEX lists both laser and waterjet cutting among the processing options available for Alloy 625 heat shield projects.
The appropriate method depends on the blank geometry, material thickness, required edge condition and subsequent operations.
Do not assume that every profile should automatically use the same cutting process.
When the cutting method is important to the drawing or downstream process, specify the required result rather than only naming the machine:
The production trial should confirm that the chosen cutting route produces blanks suitable for the next forming operation.
A cut edge that will later become a bend, flange or mounting tab deserves closer inspection than an edge that will be removed during final trimming.
Potential issues include:
The blank drawing should distinguish final edges from temporary process edges.
BSTFLEX p263 also supports deburred and optional folded or hemmed edge configurations for custom projects. Final edge requirements should be defined from the finished component drawing rather than assumed from the blank alone.
A larger blank does not automatically create a better heat shield.
Before the material outline is expanded, confirm what problem the change is intended to solve.
If the protected component remains too hot, investigate:
The flat blank should follow an approved thermal geometry. It should not become the primary method for experimenting with thermal performance during production.
Material utilization becomes particularly important when working with a nickel alloy such as Alloy 625.
For volume production, evaluate the blank layout before finalizing the incoming sheet format.
Consider:
Do not compare suppliers only by price per kilogram or price per sheet.
A more useful comparison is the material cost associated with each accepted blank and, ultimately, each accepted formed heat shield.
A rectangular blank leaves more cutting and trimming work to the customer's fabrication line.
A profile-cut blank removes material before forming and can reduce downstream processing when the component design is stable.
| Supply Form | Advantages | Points to Consider |
|---|---|---|
| Rectangular blank | Simple purchasing format and flexibility during development | More customer-side cutting and potentially greater scrap |
| Profile-cut blank | Closer to the production shape and reduces downstream material removal | Requires a controlled blank drawing and stable geometry |
| Blank with holes and slots | Can reduce downstream operations | Feature locations must remain correct after forming |
| Finished formed shield | Delivered closer to installation condition | Requires complete component and acceptance specifications |
A blank is most suitable when the customer already has the equipment and process required for forming.
A finished formed shield may be more appropriate when:
BSTFLEX p263 supports both custom-cut patterns and formed shield panels. State clearly which supply stage is required when requesting a quotation.
A custom Alloy 625 blank defines only the metal starting geometry unless additional layers are specifically included.
If the heat shield also contains insulation or backing material, add a section view showing the entire layer stack.
For guidance on distinguishing these purchasing formats, see Inconel Heat Shield Foil vs Insulated Panels: What Are You Actually Ordering?.
Do not use the overall thickness of an insulated assembly as the blank thickness of the Alloy 625 facing.
Once a prototype produces an acceptable formed shield, record the exact blank revision used.
The approval package should identify:
If the production blank later changes, the effect on the finished component should be reviewed before the new revision is released.
This is particularly important when a supplier modifies the blank to improve nesting or reduce scrap. A lower material cost is useful only if the new blank continues to produce an acceptable heat shield.
| Drawing Field | What to Specify |
|---|---|
| Material | Alloy 625 / UNS N06625 and applicable specification where required |
| Material condition | Required supply condition or approved equivalent |
| Base-metal thickness | Nominal gauge and tolerance |
| Surface | Smooth, embossed or dimpled |
| Pattern | Pattern reference, profile and orientation where controlled |
| Blank outline | Complete flat profile with controlled dimensions |
| Datums | References used to locate critical features |
| Holes and slots | Dimensions, position and manufacturing stage |
| Tabs | Outline, bend line and final function |
| Allowances | Areas required for forming, trimming or workholding |
| Edge condition | As-cut, deburred or other defined requirement |
| Quantity | Prototype and expected production volume |
For a custom Inconel heat shield blank quotation, send more than the flat drawing whenever possible.
A useful RFQ package includes:
When the blank is being developed from an existing shield, provide the physical sample together with any available original material information. A worn or distorted sample should not automatically become the new dimensional master.
It is a flat or partially prepared Alloy 625 profile intended for later forming or assembly into a heat shield. The blank can include the outside profile, holes, slots and mounting tabs according to the manufacturing process.
Yes. BSTFLEX p263 supports custom-cut patterns and project-specific processing. The required material, thickness, dimensions, pattern, tolerances and quantity should be provided for quotation.
Yes, when they are suitable for the manufacturing sequence. Their finished positions should be validated after forming if surrounding material is bent or drawn.
Yes. Embossed or dimpled surface options are available for project review. The blank drawing should identify the pattern and orientation where these are controlled.
There is no universal percentage. The required allowance depends on the component geometry, material thickness, bend or forming method, tooling and whether the part will be trimmed after forming.
No. A blank is the flat starting profile. A finished shield has already undergone the specified forming and finishing operations.
Yes. The current Alloy 625 heat shield product supports both custom-cut patterns and formed panels based on project drawings and requirements.
BSTFLEX supplies Alloy 625 Inconel Heat Shield material for custom exhaust, turbocharger, manifold, catalytic converter and other high-temperature thermal protection projects.
For a blank quotation, send the flat profile and finished-part drawing together. Include the Alloy 625 specification, base-metal thickness, embossing requirement, hole and slot details, required edge condition and prototype quantity.
If you require a fully formed metal component rather than a flat blank, also review the BSTFLEX Metal Stamping Heat Shields capability and identify the complete manufacturing scope in the RFQ.
Where Alloy 625 is not required for the application, alternative materials include embossed stainless steel heat shield material and embossed aluminum thermal barrier sheet. Material substitutions should be based on the actual thermal and mechanical requirements.
Send your Inconel heat shield blank drawing and RFQ to BSTFLEX for material, cutting, prototype and OEM production review.
No.10, Chuangxin North Road, Nanshan Park, Ningguo Economic and Technological Development Zone, Ningguo City, Anhui Province, China
teléfono/Whatsapp : 0086-15856303740
Email : sales@bstbraidedsleeve.com
Skype : vanesa-cheng