Qué buscas?
A diesel particulate filter heat shield has to work in an environment that changes repeatedly between cold start, normal exhaust operation, regeneration and shutdown. It may also sit underneath a truck or machine where vibration, moisture, road contamination and limited installation space are part of everyday service.
For that reason, DPF heat shield material should not be selected from a temperature number alone. The finished shield must protect nearby components while retaining its geometry, attachment integrity and required clearance through the complete operating cycle.
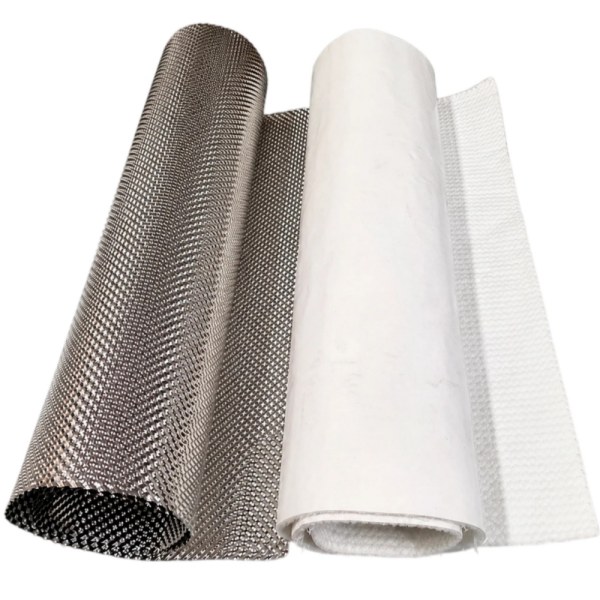
BSTFLEX supplies embossed stainless steel heat shield material for custom exhaust and diesel aftertreatment thermal barriers. The material can be cut, folded, stamped and formed according to the required DPF, DOC, exhaust pipe or underbody shield geometry.
A diesel particulate filter captures particulate matter from the exhaust stream. During regeneration, accumulated soot is oxidized using elevated exhaust-system temperatures.
This creates a thermal-management problem that differs from a conventional low-temperature body panel. The aftertreatment assembly can be located close to:
The purpose of a DPF heat shield is to control the heat reaching these surrounding components without interfering with the operation, inspection or maintenance of the aftertreatment system.
These terms are often used together, but they can describe different constructions.
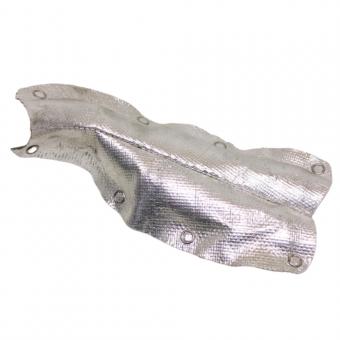
A DPF heat shield may be a separate formed metal barrier positioned around or beside the aftertreatment component.
DPF insulation may refer to an insulating layer incorporated into a multi-layer shield or other thermal assembly.
A purchasing drawing should therefore establish whether the requirement is for:
These products can contain similar metal materials but have very different thickness, manufacturing and thermal-performance requirements.
Stainless steel is a practical material family for diesel aftertreatment shielding because the application combines thermal exposure with structural and environmental demands.
A DPF shield may experience:
These requirements make mechanical durability important alongside thermal performance.
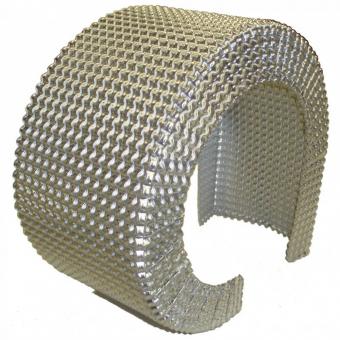
The BSTFLEX Stainless Steel Thermal Barrier Sheet uses an embossed structure rather than a completely flat surface. This geometry can improve the rigidity of thin metal and help the finished shield retain its shape after cutting and forming.
An RFQ stating only “stainless steel DPF heat shield” does not completely define the material.
The stainless grade affects properties such as:
If the vehicle or equipment manufacturer has already approved a grade, include that exact requirement in the drawing and purchase specification.
If material selection remains open, provide the operating environment and application requirements so candidate grades can be reviewed before sampling.
Do not substitute one stainless grade for another solely because both are described commercially as heat-resistant stainless steel.
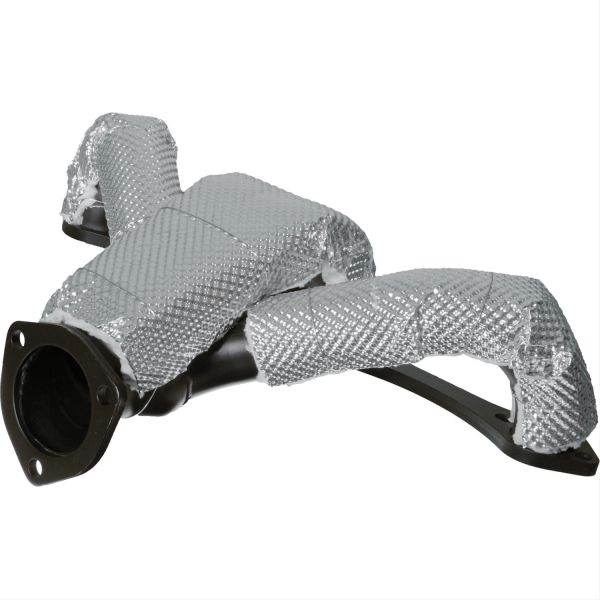
The location of the shield changes its thermal duty.
A shield located close to the DPF housing sees a more severe thermal environment and normally requires careful consideration of material grade, attachments, thermal expansion and local clearances.
A shield attached to the chassis or floor structure can be farther from the DPF and act primarily as a radiant barrier protecting the vehicle body and nearby systems.
Where a single metal layer cannot achieve the required protected-side condition within the available packaging space, an insulation layer can be incorporated into the assembly.
These three designs should not share the same material specification without engineering review.
A metal heat shield should not be evaluated independently of its installation gap.
When the metal is separated from the DPF or exhaust surface, the design can limit direct conductive heat transfer and use the sheet primarily as a radiant barrier.
If the metal is placed directly against the hot component, that contact creates a conductive path.
This means that two shields made from the same stainless steel can perform differently simply because one has an effective air gap and the other does not.
The drawing should therefore define:
Check the minimum clearance with the exhaust system hot and under the expected vehicle movement, not only when the system is cold in the workshop.
Large flat areas of thin stainless sheet can flex relatively easily. Increasing metal thickness can improve stiffness, but it also increases mass and material use.
Embossing adds three-dimensional geometry to the sheet and can improve structural stability without relying only on a heavier base-metal gauge.
For diesel aftertreatment heat shields, an embossed structure can support:
The embossing pattern must remain compatible with the subsequent forming operation. Areas around tight bends, holes or mounting interfaces may require different tooling consideration from the broad center of the panel.
| Construction | Typical Design Role | Main Items to Specify |
|---|---|---|
| Single embossed stainless steel layer | Rigid radiant barrier with controlled spacing | Grade, gauge, pattern, geometry, air gap and mounting |
| Double metal layer | Creates additional separation within the shield assembly | Inner and outer skins, spacing, joining and edge construction |
| Stainless facing plus insulation | Adds thermal resistance where a metal barrier alone is insufficient | Facing, insulation material, thickness, backing and edge closure |
| Fully formed insulated assembly | Application-specific thermal protection ready for installation | Complete drawing, interfaces, thermal requirement and acceptance criteria |
Do not transfer the temperature capability of the stainless steel directly to the insulation, backing, fasteners or completed assembly. Each layer must be suitable for its own operating condition.
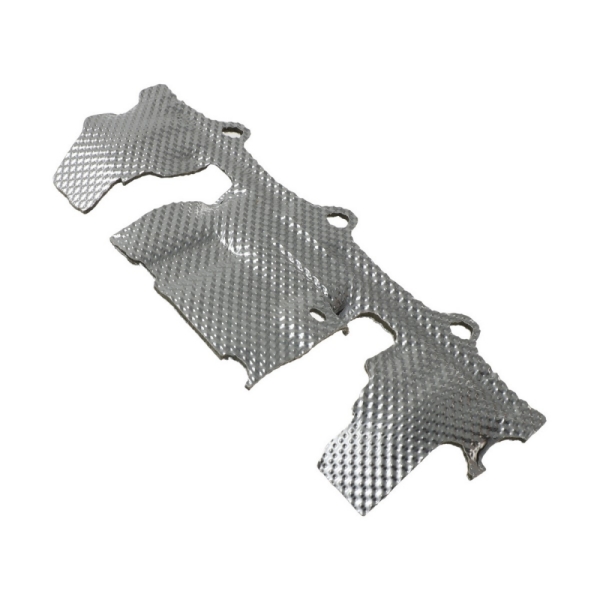
A DPF heat shield should not be validated only during steady-state engine operation.
The test program should represent the relevant aftertreatment duty cycle, including the conditions that create the highest shield or protected-component temperature.
Depending on the vehicle program, this may include:
Do not assume the hottest condition occurs while the vehicle is moving. Reduced airflow after a duty-cycle change or shutdown can alter temperatures around the aftertreatment assembly.
Heating changes the dimensions of exhaust components and their shields. Cooling reverses that movement.
If a stainless steel shield is heavily restrained at several mounting points, repeated expansion and contraction can create local stresses around tabs, fasteners, bends or holes.
The mounting design should therefore consider thermal movement as well as vibration.
Useful features may include project-specific:
These are design options, not universal requirements. Their dimensions and use must be developed for the actual shield.
An air gap around the main panel does not prevent heat conduction through a bracket or fastener connected to a hot exhaust component.
During a DPF shield review, trace the complete heat path through:
If a protected component remains too hot even though the broad shield surface performs well, a conductive attachment can be one of the areas requiring investigation.
Many diesel aftertreatment systems are positioned underneath commercial vehicles, buses, construction equipment or other machinery.
The shield can therefore face conditions that do not exist in a protected laboratory thermal test.
Depending on the application, validation may need to consider:
A material that passes an initial heat test should still be evaluated for the durability conditions relevant to the vehicle.
DPF systems are serviceable assemblies. A thermal shield should not turn routine inspection or filter service into an unnecessary disassembly operation.
Before finalizing the shield outline, identify access requirements for:
If a shield must be removed during normal maintenance, the attachment design should support repeat installation without uncontrolled deformation.
Service access should be shown on the assembly drawing rather than discovered after the first production shield is installed.
Modern diesel aftertreatment can include several components such as the diesel oxidation catalyst, diesel particulate filter and selective catalytic reduction system.
Do not use “DPF shield” as a generic name for every thermal barrier in the complete aftertreatment assembly.
For an OEM drawing, identify the actual location:
This makes supplier discussions more precise and helps keep different thermal zones from being treated as one identical material requirement.
A conventional exhaust pipe shield primarily addresses the heat produced by the exhaust flowing through a pipe. A DPF-area shield is part of a larger aftertreatment environment that can experience changing thermal conditions associated with filter operation and regeneration.
For this reason, a pipe-shield specification should not automatically be copied onto the DPF assembly without reviewing:
For broader exhaust thermal-management options, see the BSTFLEX Exhaust Heat Shield Insulation range.
The supply stage should be identified before quotation.
Raw material: embossed stainless steel sheet supplied for the customer's own cutting and forming.
Cut blank: a defined flat profile ready for subsequent forming.
Formed component: a three-dimensional metal shield with the required bends, holes, tabs and edges.
Insulated component: a complete shield containing metal and thermal insulation layers.
If a finished stamped component is required, customers can also review the BSTFLEX Metal Stamping Heat Shields range.
| Drawing Item | Required Information |
|---|---|
| Material | Stainless grade and applicable material specification |
| Base-metal thickness | Nominal gauge and tolerance |
| Embossing | Pattern reference, orientation and controlled profile requirements |
| Finished geometry | Overall outline, curved surfaces, flanges and formed features |
| Mounting | Holes, slots, tabs, brackets and attachment datums |
| Clearance | Required spacing from the DPF and surrounding components |
| Edges | Trimmed, deburred, returned, folded or other specified condition |
| Layer construction | Single layer, multiple metal layers or metal plus insulation |
| Heat-source side | Clearly marked orientation |
Material suppliers can evaluate a project more effectively when the thermal requirement describes the installation rather than providing one isolated temperature.
Useful information includes:
Identify which values are measured, calculated or estimated. This prevents an early development assumption from later being treated as a verified production requirement.
Material certificates establish information about the supplied metal. They do not demonstrate the thermal performance of the installed DPF shield.
Vehicle or equipment validation should examine the complete assembly.
Thermal performance: measure the protected components under the agreed duty cycle, including regeneration-related conditions where applicable.
Mechanical durability: inspect tabs, holes, seams and the free-state shape following the required cycling and vibration exposure.
Clearance: verify that the shield does not contact the DPF, exhaust piping or adjacent systems throughout operation.
Environmental durability: evaluate corrosion or contamination where relevant to the installation.
Serviceability: confirm that required sensors, clamps and filter-service interfaces remain accessible.
Stainless steel is widely suitable for DPF and diesel aftertreatment heat shielding because these applications can combine high thermal exposure, vibration and underbody environmental conditions. The exact stainless grade and shield construction should be selected for the specific system.
A DPF operates in a high-temperature exhaust environment and can experience elevated thermal loads during regeneration. A heat shield helps control heat exposure to surrounding vehicle or equipment components.
Aluminum can be considered for some secondary or body-mounted radiant barriers where the measured thermal conditions permit it. A close-fitting DPF shield should be selected from its actual operating environment rather than from weight alone.
No. Stainless steel sheet can form the metal barrier or outer skin. An insulated DPF shield also contains a separate thermal insulation layer. The complete construction should be shown in the specification.
Increasing metal thickness changes mechanical strength and stiffness, but metal gauge alone does not define thermal protection. Air gap, coverage, surface condition, insulation layers and mounting heat paths also influence performance.
Yes, when regeneration represents a relevant high-temperature operating condition for the application. The validation cycle should reproduce the thermal conditions the production shield is expected to encounter.
BSTFLEX supplies embossed stainless steel thermal barrier sheet and supports custom sheet sizes, patterns and formed heat shield projects according to drawings, samples and application requirements.
BSTFLEX supplies embossed stainless steel thermal barrier sheet for diesel particulate filter, catalytic converter, exhaust pipe and other automotive or heavy-duty thermal protection projects.
Send the aftertreatment assembly drawing, required stainless grade, base-metal thickness, embossing requirement, finished dimensions and prototype quantity. Include the DPF position, mounting layout, available clearance and operating conditions where available.
For exceptionally demanding thermal environments where a nickel alloy is under consideration, BSTFLEX also offers Alloy 625 Inconel heat shield material. The alternative should be evaluated against a defined material requirement rather than treated as an automatic upgrade.
Send your DPF heat shield drawing and RFQ to BSTFLEX for material, prototype and OEM production review.
No.10, Chuangxin North Road, Nanshan Park, Ningguo Economic and Technological Development Zone, Ningguo City, Anhui Province, China
teléfono/Whatsapp : 0086-15856303740
Email : sales@bstbraidedsleeve.com
Skype : vanesa-cheng